


Skip to content

Automate Pin Press-Fitting and Control Pneumatic Joining Processes

RXLea
Digital projects for hands-on learningInteractive learning content, directly connected to the training system.

Automate Pin Press-Fitting and Control Pneumatic Joining Processes

CIU05IU

Teach automated joining processes through hands-on training. Your students program pneumatic pin press-fitting, monitor cylinder positions, and control workpiece transport in TIA Portal.

Learning Content
  • Understanding joining processes
  • Controlling the press cylinder
  • Evaluating cylinder end positions
  • Designing HMI interfaces
KEY FEATURES
  • Precise press-fit and joining process
  • End position monitoring in both cylinder positions
  • Following the joining sequence on the touch panel
  • Smooth approach using PWM
Speak with a Product Specialist +1 (757) 808-5696 · sales@lucas-nuelle.com

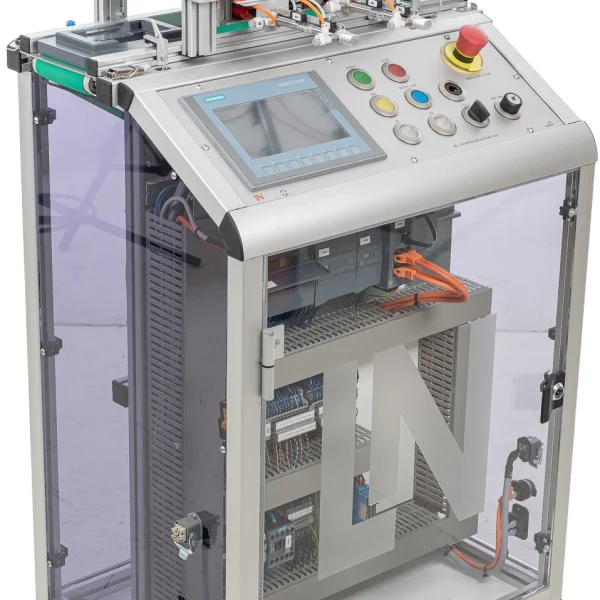
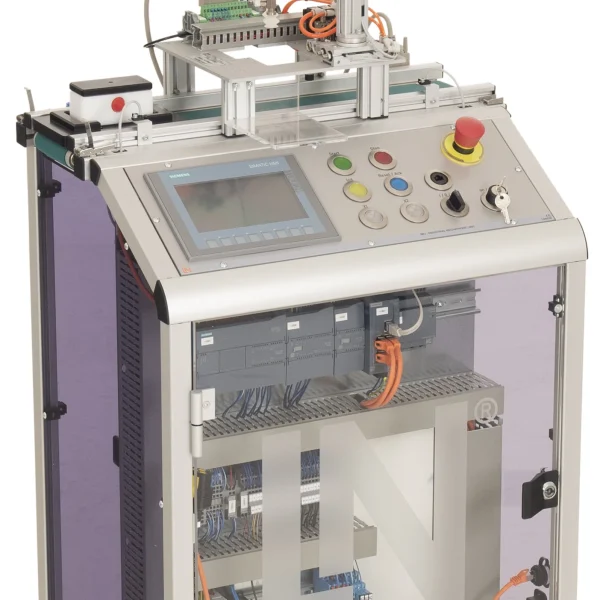
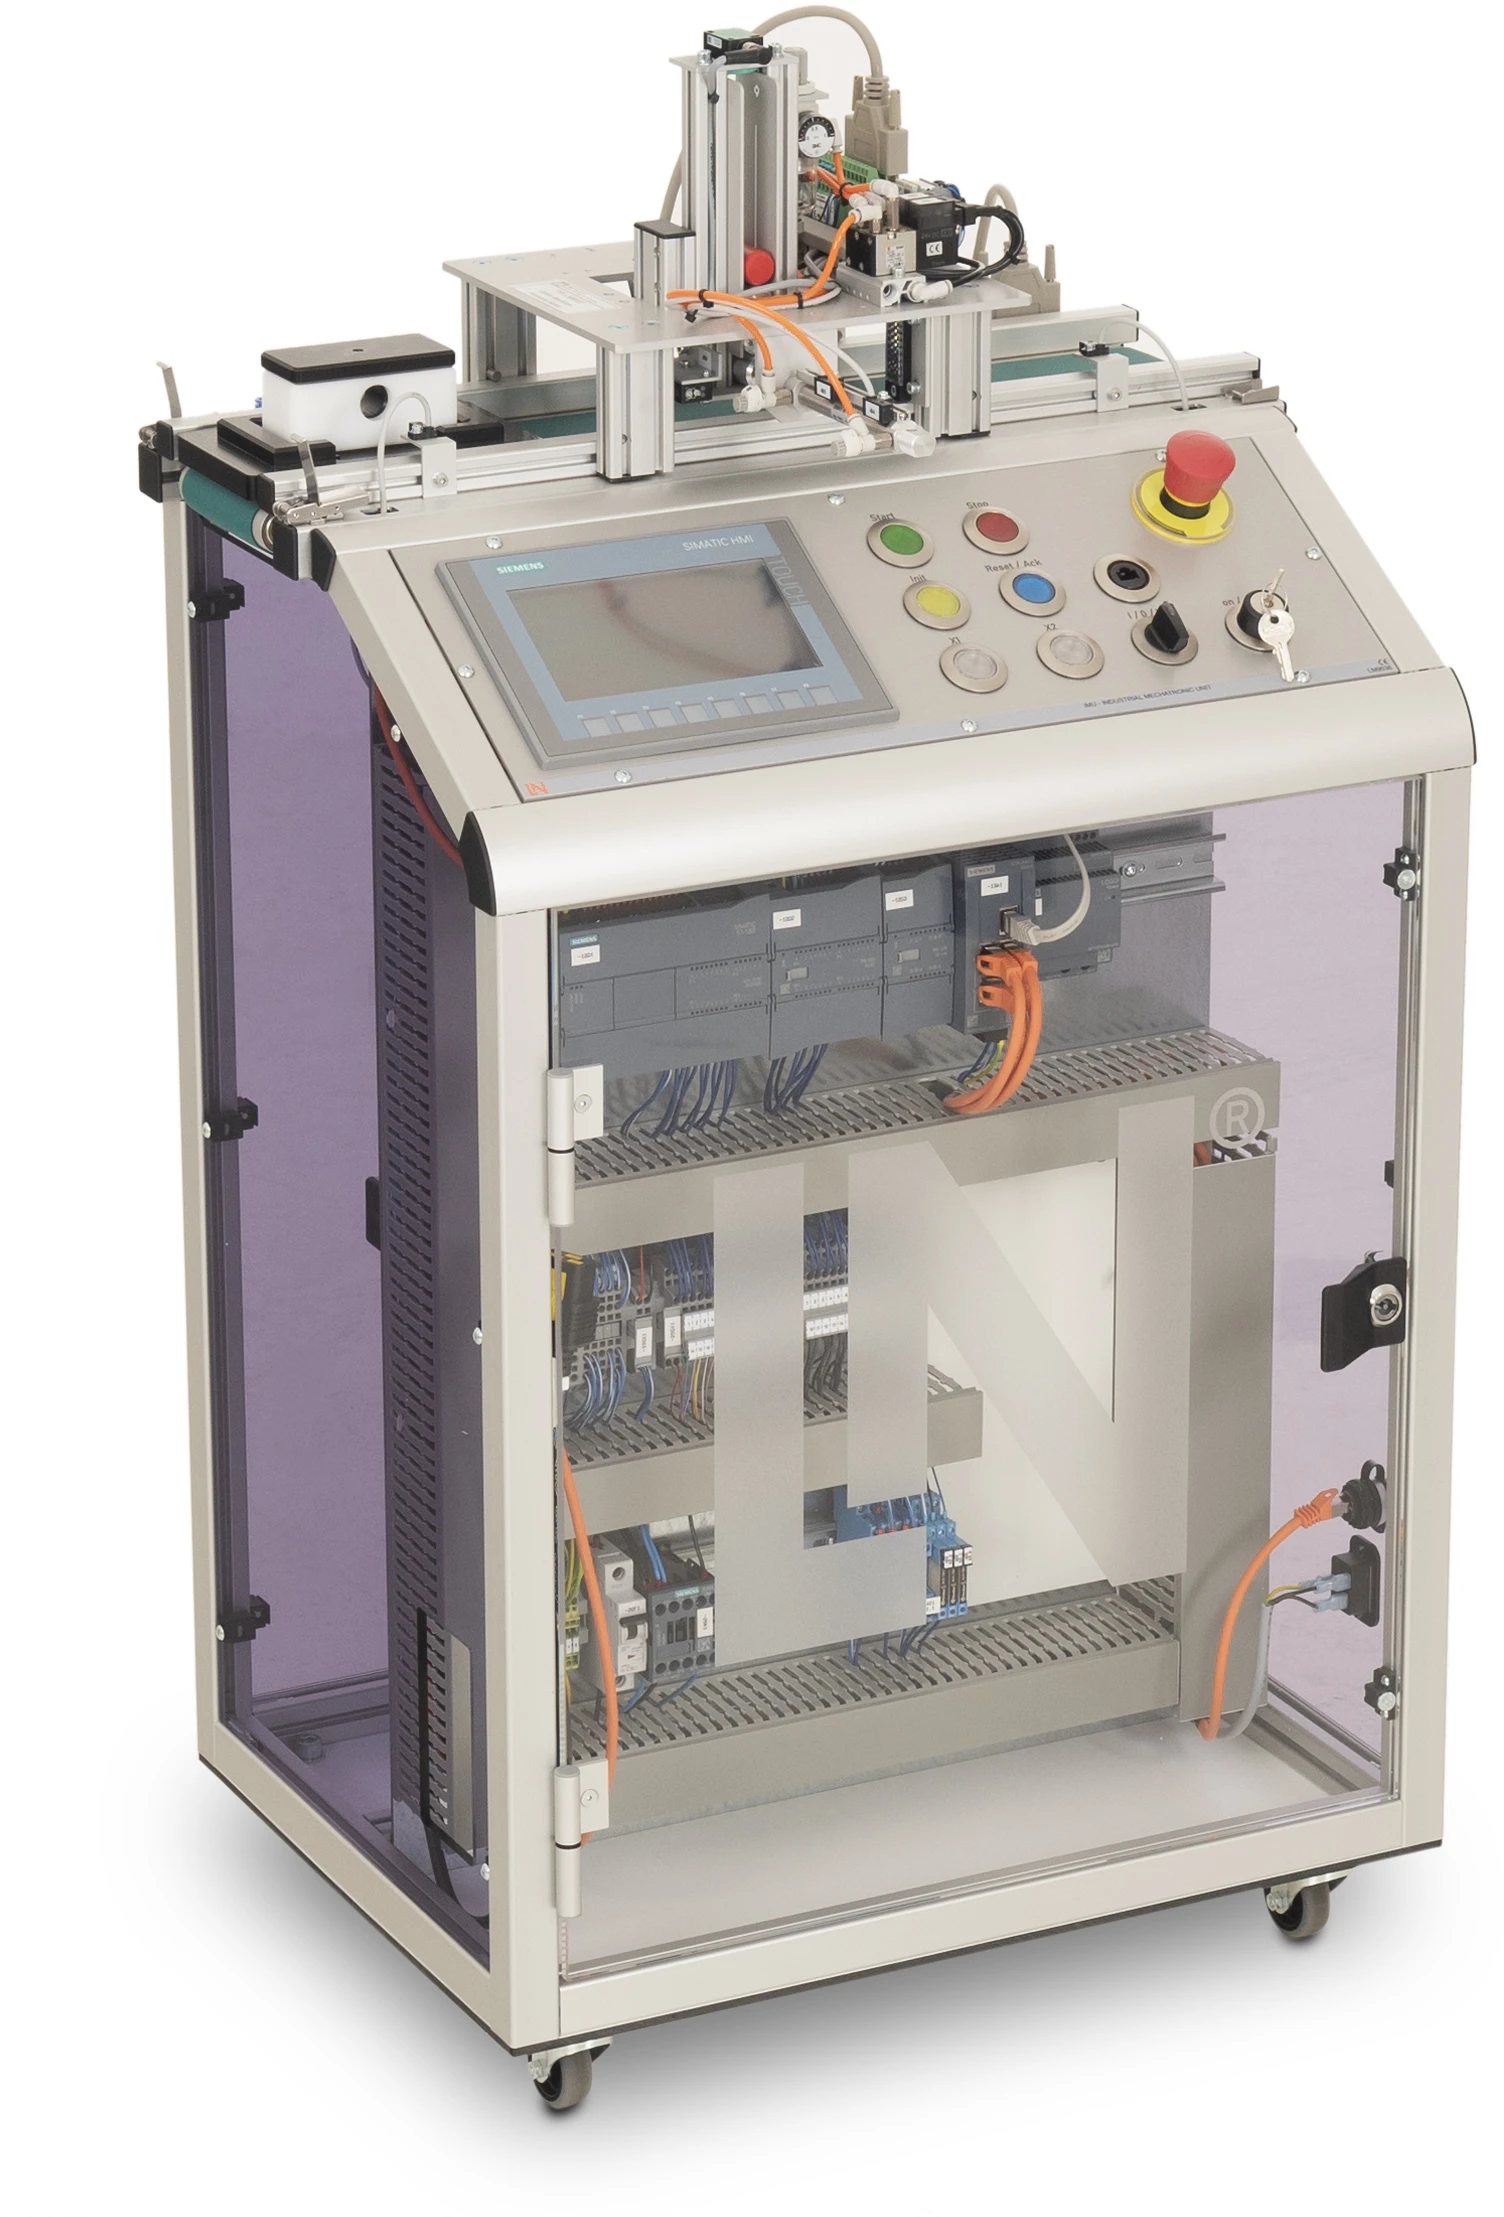
How can connecting pins be precisely press-fitted into workpieces during automated assembly? The mobile Industrial Mechatronic Unit (IMU) helps you teach your students how sequence control, pneumatics, and workpiece transport interact in a complete manufacturing station. Students program the press-fitting process, process sensor signals, and develop a graphical user interface.

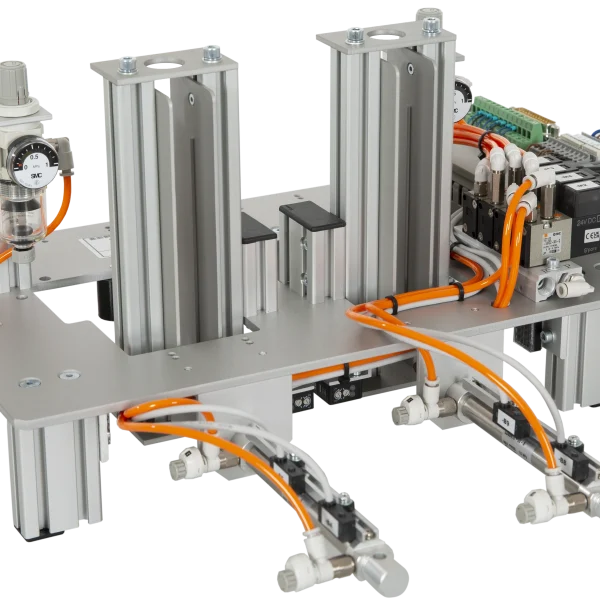
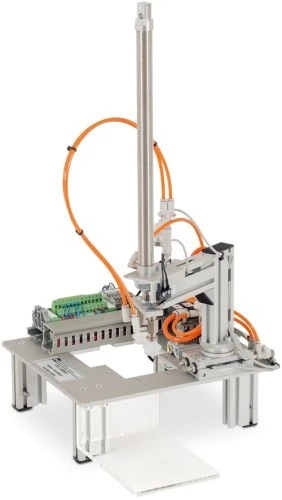
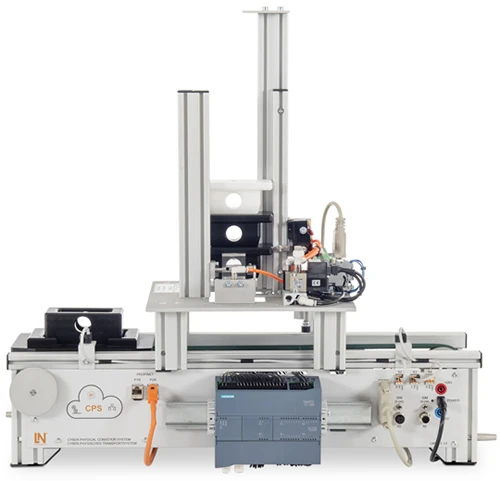
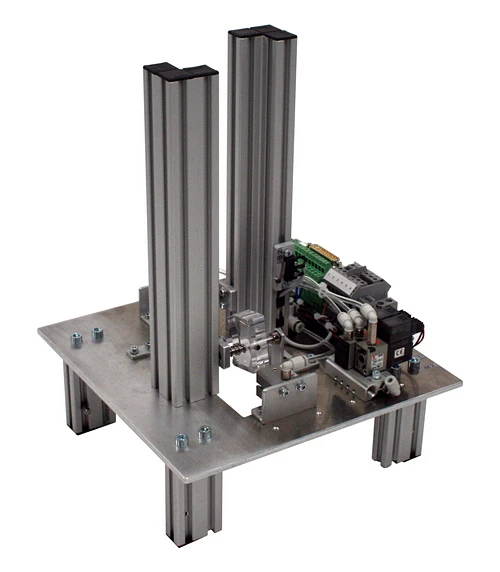
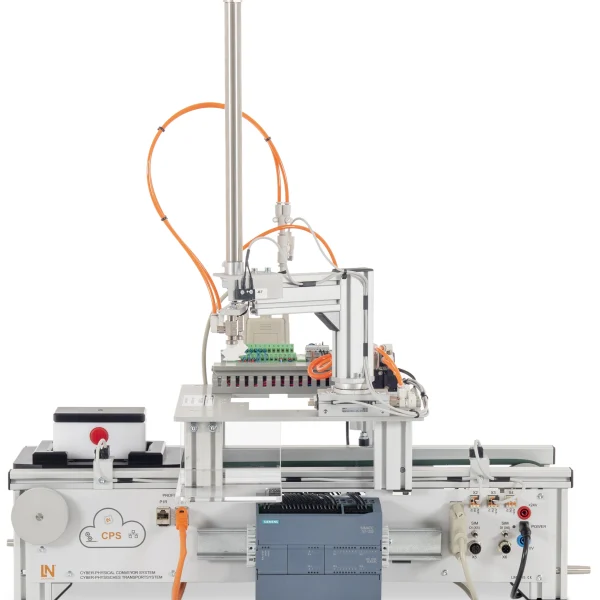
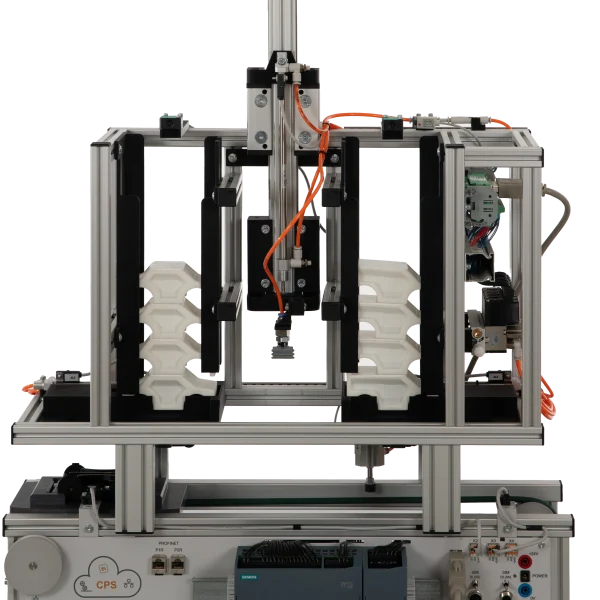
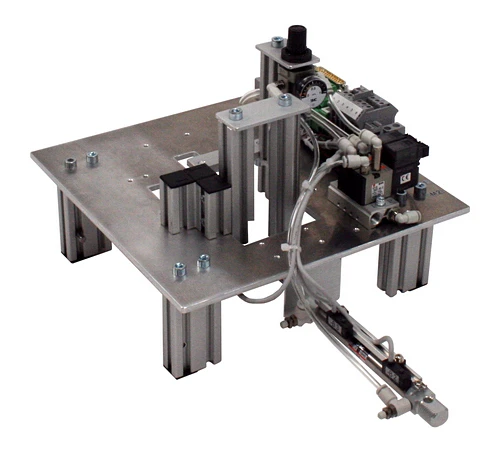
The IMU combines a conveyor system with the machining subsystem. A magazine supplies aluminum or plastic pins. The conveyor transports the workpiece carrier to the press-fitting station, where a pneumatic stopper positions it. A pneumatic press cylinder then inserts the pin into the prepared hole in the lower housing section. Two magnetic cylinder sensors monitor the home and pressing positions. The controller, touch panel, and pneumatic components are integrated into the mobile unit.

Your students develop the sequence control program for the press-fitting process in TIA Portal, evaluate the cylinder position signals, and adjust conveyor speed using pulse-width modulation (PWM). They also design the graphical user interface for the touch panel. Through these activities, they learn to coordinate workpiece transport, positioning, and pneumatic press-fitting. This helps you strengthen their understanding of automated joining processes and develop practical skills in programming, operating, and monitoring mechatronic manufacturing stations.

LM9536Industrial Mechatronic Unit
LM9532Film, for oscilloscope cameratype LM 7000
SO6200-2UQuickChart, IPA 1 Compact station (GB)
LM9682Processing station
LM9066Interface cable 25-pin, Sub-D socket / plug 1m
SO6200-1EQuickChart, IMS 5 Mechatronics Process subs-system (GB)
SO2805-5JInteractive Lab Assistant: IMU 1 Industrial Mechatronic Unit
SO2805-5XInteractive Lab Assistant: Self-commutated converter circuits
LM9525Workpiece, bottom section, black
LM9521Workpiece, top section, white
LM9527Bolt workpiece, metal
LM9528Bolt workpiece, plastic

Learning Content in Detail

Learners work through the press-fit process, from the pneumatic sequence and evaluation of the end position signals through to diagnosing incorrect positions.

Understanding joining processes

Learners analyze the pneumatic and mechanical sequence involved in press-fitting pins into assemblies.

Controlling the press cylinder

Learners program the solenoid valves for precise timing of the ejection and press-fit operations.

Evaluating cylinder end positions

Learners logically process the signals from the magnetic cylinder switches in the home and pressing positions.

Designing HMI interfaces

Learners design touch panel screens for process control and status display.

Controlling speed via PWM

Learners configure the pulse generators of the S7-1200 to adjust the conveyor speed smoothly.

Integrating magazine monitoring

Learners link the retro-reflective light barriers so that the process switches off automatically when a chute is empty.

Creating modular function blocks

Learners encapsulate the press-fitting logic in reusable blocks with clearly defined interfaces.

Carrying out fault diagnosis

Learners identify misaligned cylinder switches and malfunctions in the sequence code.

Features & Applications

The unit covers automation technology, joining and press-fit technology, and industrial control technology.
  • Precise press-fit and joining process — The subsystem pushes pins from the supply magazine into the prepared bore in the housing with a precise fit and controlled cylinder force.
  • End position monitoring in both cylinder positions — Two magnetic cylinder switches monitor the home position and the extended press position of the working cylinder.
  • Following the joining sequence on the touch panel — The KTP700 touch panel displays the joining sequence and the sensor states in real time and enables manual process control.
  • Smooth approach using PWM — The PLC reduces the conveyor speed ahead of the stopper using pulse-width modulation and positions the carrier exactly beneath the press.
  • DC motor with incremental encoder — The drive enables speed-controlled conveyor movements as well as distance and position measurements by evaluating the pulses.
  • Siemens S7-1215C with digital module — The PLC coordinates the conveyor motor, stopper and press cylinder while recording current and voltage values.
  • SIMATIC KTP700 Basic Panel (CO3713-4Q) — On the panel, learners develop HMI interfaces for process monitoring and for adjusting parameters.
  • Magazine for press-fit pins — The magazine holds aluminum or plastic pins and feeds them to the press-fit mechanism by gravity.
  • IO-Link with RFID head and ultrasonic sensor — An RFID read/write head connected via the IO-Link master module writes data to and reads data from the workpiece carrier. The ultrasonic sensor outputs the precise fill level of the magazine.
  • Siemens TIA Portal and WinCC — Engineering environment for blocks, step sequences and HMI screens for the joining process.
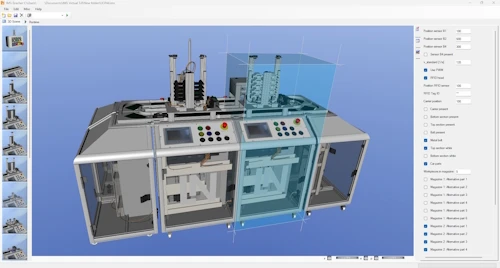
  • Interactive Lab Assistant course SO2805-5J — Interactive learning software with step sequence instructions, 3D models and automated knowledge tests.
Learners working with RXLea on a tablet at a Lucas-Nuelle training system
RXLea

From Knowledge Comes Capability.

You guide the learning

Where theory and practice go hand in hand.

RXLea brings a new way of learning: project-based, hands-on and clearly structured. Learners solve real-world tasks, while instructors save time on preparation. Interactive modules, smart analytics and real hardware create a modern, efficient learning world.

Hands-on and interactive

Animations, interactive tasks and realistic scenarios build a deep understanding. All content is organized into clear learning paths for focused, hands-on learning.

Digital support

3D assembly animations and digital instructions simplify complex procedures, reduce errors and help learners work more independently.

Visual support

Overview graphics, screenshots and sample animations make the learning world transparent. Photos from the learning packages are also available, including country-specific versions where needed.


Learners using a tablet at an energy training system
RXLea on desktop, laptop and tablet
RXLea Path Creator for building learning journeys
RXLea Navigator showing the learning world
Learn more about RXLea
Newsletter

Stay ahead in
technical training.

Get the latest training systems, product launches and educational insights, delivered directly to your inbox.

Your email address

By subscribing, you agree to our Privacy Policy. You can unsubscribe at any time.

 Please select at least one category before subscribing.
I'm interested in - select all that apply